 English
 русский
 Français
 Español
 عربى
Actualités de l'industrie
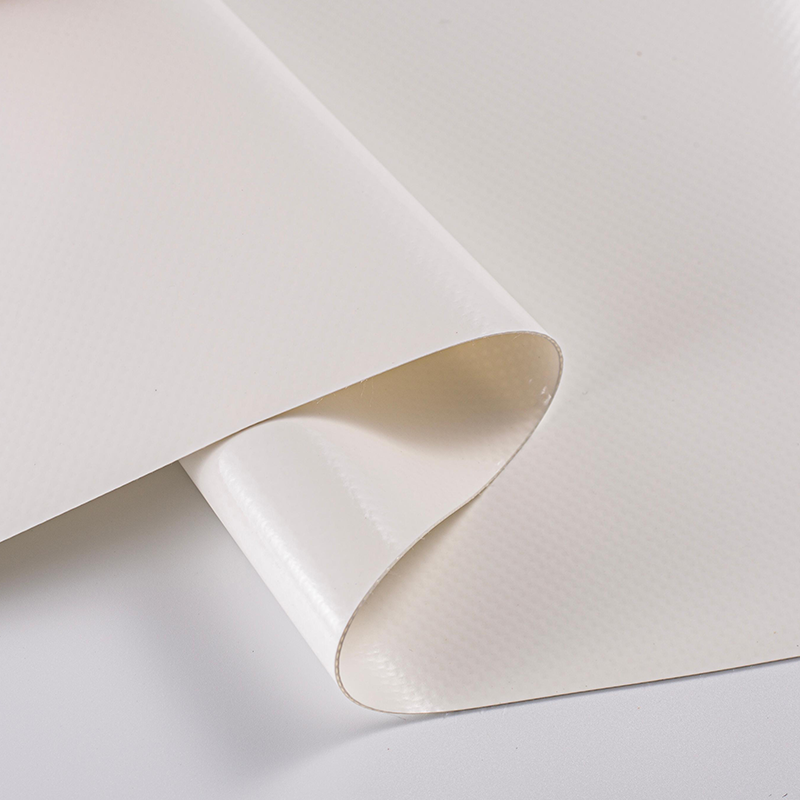 Acrylic-Coated PVC Architectural Membrane Fabric JT-1050A 1050 g/m² double-sided PVC membrane with acrylic surface protection, suited to canopies, shade structures and tensile roofs where weldable, weather-resistant fabric is needed.View Product →
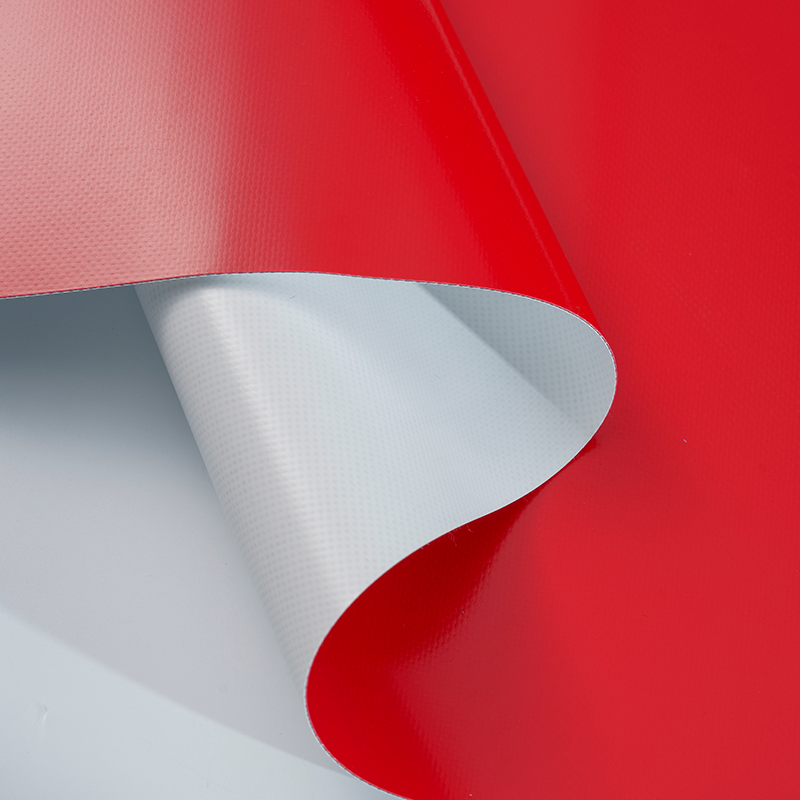 PVDF-Coated PVC Architectural Membrane JT-1200A 1200 g/m² PVC membrane with PVDF and acrylic topcoat for tensile roofs and facades where anti-fouling and colour retention reduce maintenance demands.View Product →
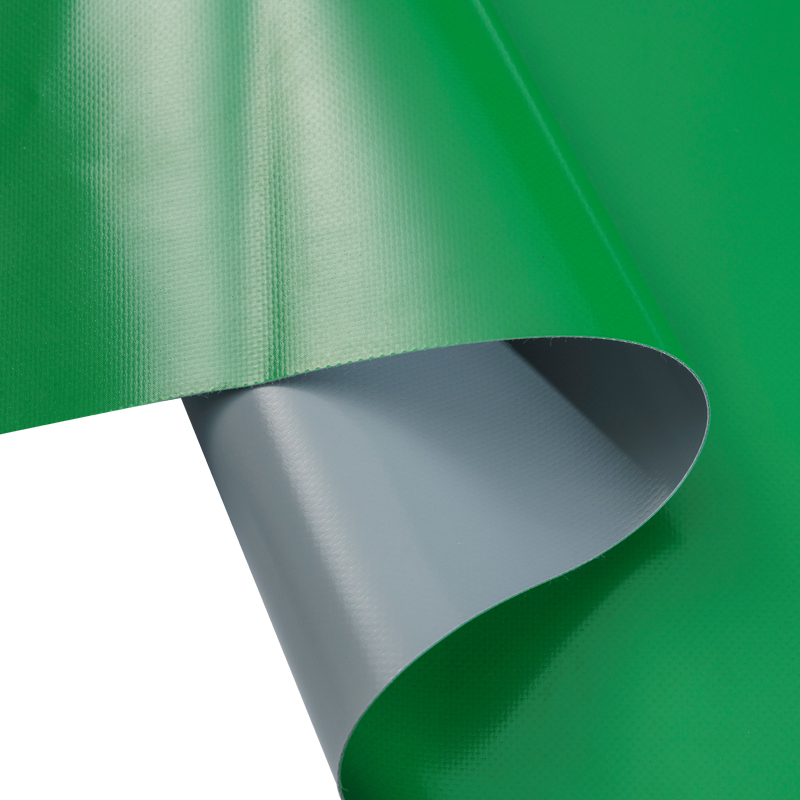 1000D 850gsm PVC Coated Fabric for InflatablesA heavy-duty 850 g/m² double-sided PVC fabric on 1000D polyester, suited to large inflatables and air-supported structures that need strength and repeated packing.View Product →
Made in USA ETFE vs Coated PVC Membrane: Sourcing Guide for B2B Buyers
Content
- 1 What Made in USA ETFE Actually Covers in a Specification
- 2 ETFE Film and Coated PVC Membrane Side by Side
- 3 Where Each Material Earns Its Place
- 4 When the Origin Requirement Is the Real Driver
- 5 Coating Systems Decide What Your Membrane Looks Like After Five Summers
- 6 Reading Fabric Weight Before You Commit to a Substitution
- 7 Sampling, Minimum Order and Lead Time: What a Manufacturer Owes You
- 8 A Submittal Checklist for Mixed-Origin Projects
- 9 Matching the Fabric to the Application
- 10 FAQ: Made in USA ETFE and Coated Fabric Sourcing Questions
- 10.1 Is made in USA ETFE the only compliant option for a federally funded envelope?
- 10.2 Can coated PVC membrane replace ETFE cushions on an existing design?
- 10.3 What documents should support an ETFE origin claim?
- 10.4 How much heavier is a coated PVC membrane than ETFE film?
- 10.5 Can a manufacturer based in China supply into a US project?
- 10.6 What lead time should I plan for coated PVC fabric?
- 10.7 Which coating should I choose for a fifteen-year appearance target?
- 10.8 Does Kingtex supply ETFE film?
- 11 Where to Go Next
A specifier in the Midwest sends out an RFQ for 6,000 m² of pneumatic cushion film. Two replies land on the same afternoon. One quotes an ETFE foil extruded in the United States, a 26-week lead time and a certificate of origin that satisfies the Buy American clause on the project. The other quotes an imported coated membrane at a fraction of the material price, with mill test reports but no domestic origin. On paper, the second offer looks like the better buy. In practice, the decision has very little to do with which polymer is superior and everything to do with which constraint is actually binding on that job.
That is the short answer: a made in USA ETFE label answers a compliance question, not a performance question. It tells you where a film was made. It does not tell you whether the cushion geometry is right, whether the weld schedule will hold for twenty years, or whether a coated fabric would have done the same job for less money and less schedule risk.
This article is written from the position of a coated-fabric mill, so the bias should be stated up front. Kingtex, the brand of Anhui Kingtex Material Technology Co., Ltd., manufactures PVC-coated and laminated fabrics in Anhui, China. We do not extrude ETFE film and we do not sell it. What we can do is explain where fluoropolymer film genuinely earns its premium, where a coated PVC membrane is the more practical answer, and what a buyer should put in writing before either material is released for production.
What Made in USA ETFE Actually Covers in a Specification
ETFE is a copolymer of ethylene and tetrafluoroethylene, extruded into film rather than woven or coated. Architectural grades usually run somewhere between 50 and 250 micrometres, printed or fritted when shading is needed, and formed into two or three-layer pneumatic cushions held by aluminium extrusions. It is a genuinely remarkable material for the right envelope, and the suppliers who make it have spent decades earning that reputation.
The phrase "made in USA" is where specifications start to blur. A single ETFE cushion assembly passes through at least four separate manufacturing steps, and each one can happen in a different country:
- Polymerisation of the resin, which may occur in Europe, Asia or North America depending on the grade.
- Extrusion of the film, which is the step most buyers mean when they say the material is American-made.
- Printing or fritting of the shading pattern, sometimes a separate facility again.
- Welding of cushions and fabrication of extrusions, which may sit with a specialist contractor rather than the film producer.
A credible origin claim should therefore be documented at each level, not averaged into a single sentence on a quotation. Ask for a certificate of origin, a mill certificate naming the extrusion plant, resin lot traceability, and a separate statement covering who welded the cushions. If a supplier can only speak to the film and not to the assembly, the compliance case is thinner than it looks.
There are usually four reasons the origin question appears at all. Federal or state funding programmes may impose domestic content thresholds. Tariff exposure can swing the landed cost of an imported film by double digits. Warranty response and replacement lead time matter enormously when a single damaged cushion can leave a public building open to the weather. And quite often, the specification simply inherited the wording from a reference project and nobody has tested whether it is still necessary.
None of those four reasons says anything about weatherability, light transmission or weld integrity. Origin is an attribute of the supply chain, not of the envelope.
An origin certificate proves where a film was extruded; it proves nothing about whether the cushion design, weld schedule or detailing will survive twenty years of UV and thermal cycling.
ETFE Film and Coated PVC Membrane Side by Side
Most procurement teams compare the two materials on price per square metre and stop there. That comparison is misleading, because the two products sit in different structural systems. A fairer exercise is to compare them attribute by attribute, then decide which attributes the project actually rewards.
| Attribute | ETFE film | Coated PVC membrane |
|---|---|---|
| Optical character | High visible light transmission, typically quoted in the low nineties as a percentage for clear film | Translucent grades pass daylight but at noticeably lower levels; opaque, printed and blackout versions are straightforward |
| Areal weight | Very light, roughly a third of a kilogram per square metre at common architectural thicknesses | Heavier, generally in the 400 to 1,100 gsm band depending on base cloth and coating build |
| Structural approach | Pneumatic cushions on a light frame; requires constant air pressure and monitoring | Tensioned membrane, hall or canopy structure, often with fewer mechanical services |
| Site fabrication | Heat welding of film under controlled conditions, usually by specialist crews | High-frequency, hot-air or wedge welding; a broader contractor base is familiar with the process |
| Surface and cleaning | Non-stick surface sheds dirt readily; cleaning cycles are infrequent | Topcoat quality drives behaviour; PVDF surfaces stay cleaner than plain acrylic coatings |
| Service life expectation | Supplier-declared figures commonly sit in the 25 to 30 year range or beyond | Supplier-declared figures commonly sit in the 15 to 20 year range, longer where topcoats and detailing are good |
| Fire behaviour | Melts and vents under fire load; behaviour is well documented in national test regimes | Flame-retardant formulations are available and widely tested; performance depends on the specific compound |
| Repair strategy | Localised patching of film is possible but usually a specialist task | Patches, replacement panels and re-tensioning are routine for local fabricators |
| Origin flexibility | Limited number of extrusion plants worldwide, so domestic origin constrains the supplier list | Wide manufacturing base across Asia, Europe and the Americas |
| Cost basis | High material cost offset by low structural weight and long life | Lower material cost, with structural steel and connection design taking a larger share of the budget |
| Typical fit | Signature civic envelopes, atria and roofs where transparency is the design idea | Industrial, agricultural, transport, leisure and large-span shading where function and budget lead |
Read the table as a set of trade-offs rather than a scorecard. The weight difference is the most consequential line. Because ETFE film is so light, the supporting structure can be dramatically slimmer, and on a long-span roof that saving can offset a large share of the film premium. On a smaller canopy or a covered walkway, that structural advantage shrinks and the material premium no longer hides inside the steel budget.
The optical line cuts both ways as well. High transmission is an asset for a daylighting strategy and a liability for a space that needs glare control, blackout or thermal discipline. A coated PVC membrane with a lighter interior face can deliver diffused light with less solar gain, and it can be printed, laminated or coated to match a colour scheme in ways that film cannot match economically.
Finally, look at who can repair the envelope. A specialist film crew may be hundreds of kilometres away, and a damaged cushion can mean weeks of temporary sheeting. A coated fabric panel can often be replaced by a regional fabricator with standard equipment. For a facility manager with a twenty-year operating budget, that difference is worth real money.
The material premium for film only pays back where the structural weight saving and the transparency are both genuinely valuable to the design.
Where Each Material Earns Its Place
ETFE strengths that are hard to replace
There are envelopes where film is simply the right answer. A transparent cushion roof over a public atrium reduces structural steel, admits daylight across a wide span and resists soiling better than almost any coated textile. Where the design intent is lightness and transparency, substituting a heavier membrane forces a structural redesign that can cost more than the film ever did. Buyers in that position should pay for the film and spend their energy on weld qualification and cushion controls.
Where coated PVC membrane makes more commercial sense
Flip the conditions and the argument reverses. If the building needs shade rather than daylight, if the span is moderate, if the envelope sits over a warehouse, a livestock shed, a sports court or a truck yard, then high light transmission is a cost with no benefit attached. Coated fabric wins on price, on the breadth of available weights, on colour and print options and on the number of contractors who can install and repair it.
Architectural membrane grades are the closest structural equivalent in our catalogue. Acrylic-coated PVC is the workhorse option for general canopies and shade structures, while PVDF-coated grades hold colour and gloss longer in polluted or coastal air.
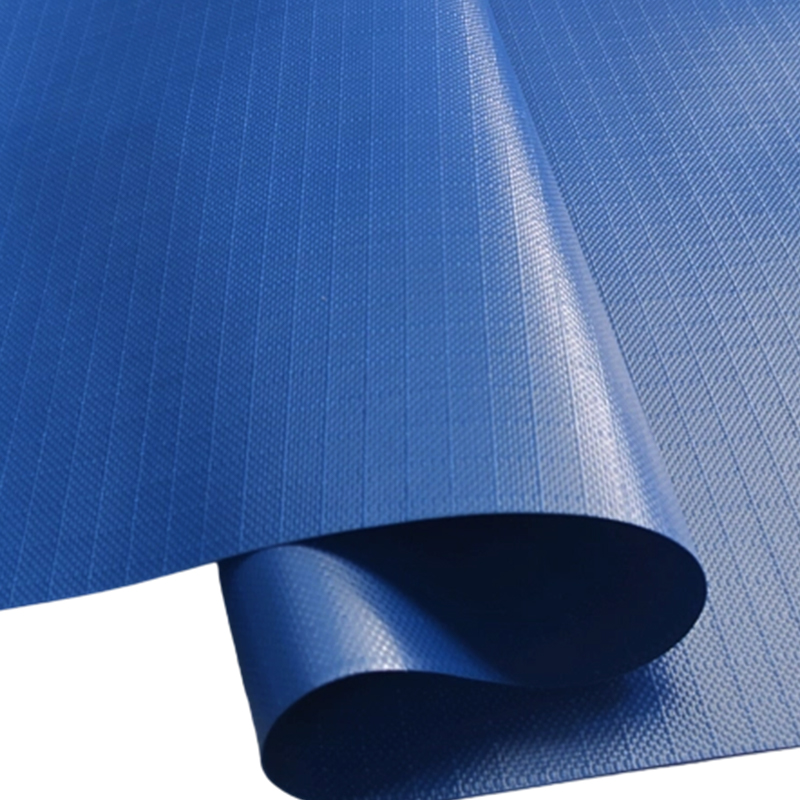
Acrylic-Coated PVC Architectural Membrane Fabric JT-1050A 1050 g/m² double-sided PVC membrane with acrylic surface protection, suited to canopies, shade structures and tensile roofs where weldable, weather-resistant fabric is needed.View Product →
Hybrid detailing deserves more attention than it gets
Mixed envelopes are common in practice and rarely discussed in specifications. A film cushion roof can sit above a coated fabric soffit or blackout layer, combining daylight at the top with glare and thermal control below. Coated fabric also serves well as a temporary enclosure during construction, when the permanent film roof is still months away from delivery. Neither role requires the two materials to compete.
Choose the material that matches the design intent, then check whether the origin clause still permits it.
When the Origin Requirement Is the Real Driver
Sometimes the polymer debate is irrelevant because the funding agreement settles the question. Domestic content rules attached to publicly funded work can require a documented percentage of American-made components, and a film extruded overseas may fail that test regardless of how well it performs. In those projects, the practical sequence is to confirm eligibility first, then optimise the design within the eligible supplier pool.
Two habits save a lot of trouble. First, check the tariff classification and the country-of-origin rule that applies to your specific product, not to the raw polymer. A film and a finished cushion can carry different origin determinations, and substantial transformation arguments need documentation rather than assumption. Second, keep the compliance file separate from the technical file. When an auditor asks why a particular roll was accepted, you want a certificate of origin and a mill certificate sitting side by side, not buried in a folder of drawings.
If the domestic content threshold is strict, a fabric produced in China will not satisfy it, and no amount of technical equivalence changes that. Kingtex states its manufacturing origin plainly and provides mill certificates, batch records and declaration documents for each shipment, so buyers can make the compliance call with accurate information rather than optimistic sales language.
Where the clause applies only to the visible envelope, a sensible split is film for the public-facing roof and coated fabric for interior liners, service corridors, temporary works and secondary canopies. Documenting the two scopes separately keeps the compliance argument clean and usually trims the budget at the same time.
Resolve the origin question before the design is frozen; retrofitting a domestic content requirement into a completed specification is expensive and slow.
Coating Systems Decide What Your Membrane Looks Like After Five Summers
If the project lands on coated PVC, the next decision matters more than most buyers expect. The base cloth sets the strength; the coating system sets the appearance, the cleaning interval and the useful life. Three families dominate architectural work.
Acrylic-coated PVC is the general-purpose choice. It welds predictably, comes in a wide colour range and handles typical canopy duty well. Its weakness is surface behaviour: over several seasons, dirt accumulates and the gloss drops, so the roof looks older than its structural condition suggests.
PVDF-coated PVC adds a fluoropolymer top layer that resists dirt pickup and holds colour. On a building where access for cleaning is awkward, or where the envelope is the public face of the site, that topcoat often pays for itself in maintenance savings alone. Industrial-grade PVDF goes a step further on coating build and is specified where the environment is aggressive or where recoating is simply not an option.
PVDF-Coated PVC Architectural Membrane JT-1200A 1200 g/m² PVC membrane with PVDF and acrylic topcoat for tensile roofs and facades where anti-fouling and colour retention reduce maintenance demands.View Product →
Three questions will settle most coating arguments. How often can the owner realistically clean the roof? What colour retention target has to be met at year ten? And what does a replacement panel cost compared with a premium topcoat at day one? When the answers point to difficult access and a visible location, the higher-grade coating is usually the cheaper decision across the life of the building.
Specify the coating by maintenance reality, not by catalogue tier; a premium topcoat on an inaccessible roof is one of the few upgrades that reliably repays itself.
Reading Fabric Weight Before You Commit to a Substitution
Once a project moves from film to coated fabric, the specification shifts from optical performance to grams per square metre, base cloth denier and coating build. Those numbers are not interchangeable between product families, and the range of options available tells you how precisely a supplier can match your duty cycle.
The chart below counts the documented specification variants within each PVC product family in the Kingtex catalogue. It is a measure of selection granularity, not of quality: a family with more variants simply offers more levers to pull on weight, weave and coating.
Documented specification variants per PVC product family
Truck cover and side curtain
5
Inflatable fabric
4
Tent fabric
4
Cover material
3
Architectural membrane
3
PVC mesh fabric
1
The truck cover family carries the widest spread, from a 400 gsm rib-stop fabric up to a 900 gsm side curtain grade, because the duty cycle varies so much between a curtain-side trailer and a tipper working on abrasive loads. Inflatable fabric runs from 550 gsm double-side coated cloth to a 900 gsm Panama weave, which gives an inflatable producer room to trade weight against stiffness and air retention. Cover material sits in a tighter band between 550 and 750 gsm, since most tarpaulin jobs are settled by handling weight and abrasion rather than by extreme loads.
For a buyer coming from a film specification, the practical lesson is to stop asking for a single equivalent product and start describing the load case. Tell the manufacturer what the fabric has to resist, how it will be handled, whether it will be folded or kept under tension, and how long it needs to last. A supplier with a broad catalogue can then propose two or three realistic options, and a wholesaler or distributor with stock can often shorten the delivery path for the lower-weight grades.
It is worth adding that no weight figure substitutes for test data. Ask for tensile and tear results on the actual batch, not on a generic datasheet, because coating adhesion and base cloth quality vary between mills even at identical grammages.
Describe the duty cycle rather than naming a product; the right grammage follows from the load case, not from a conversion table.
Sampling, Minimum Order and Lead Time: What a Manufacturer Owes You
The gap between a good quotation and a good delivery is usually paperwork. Before releasing a coated fabric order, insist on a sample cut from a production lot rather than a bench sample, and ask which lot it came from. Confirm that the sample matches the colour standard under a stated light source, because a match under office lighting can look wrong on a roof.
On commercial terms, four points deserve a written answer. What is the minimum order quantity per colour, and does it change if the colour is a custom match? What is the lead time measured from deposit rather than from enquiry? What are the roll dimensions, core diameter and packing method, since unsuitable rolls cause waste at the cutting table? And what test reports accompany the shipment, signed and dated?
Payment structure matters as much as price on a first order. A supplier confident in its process will usually accept a deposit plus balance against documents, and will not object to a pre-shipment inspection. Buyers sourcing from a new manufacturer should also ask whether the mill can supply the same base cloth across repeat orders, since a silent change of greige goods is one of the most common causes of performance drift.
Kingtex operates coating, cold lamination and hot lamination lines with in-house testing equipment, and invites buyers to visit the plant before committing to volume. For a first order from a new region, that visit or a third-party inspection is a better risk control than any discount.
Get the sample provenance, the lot number and the packing specification in writing before the deposit leaves your account.
A Submittal Checklist for Mixed-Origin Projects
Projects that combine domestic film with imported coated fabric fail on documentation far more often than on material quality. The list below covers the items that auditors and consultants ask for most frequently.
- Certificate of origin for every component, broken down by manufacturing step rather than issued as a single blanket statement.
- Mill certificates showing base cloth, coating type, grammage and batch number for each roll delivered.
- Test reports for tensile strength, tear resistance, coating adhesion and flame performance, referencing the standard used.
- Colour approval records with the light source and tolerances stated, plus retained physical samples.
- Weld procedure qualification for the fabric actually supplied, not a generic procedure from a different grade.
- Packing list with roll numbers that map back to the batch records.
- A maintenance note describing cleaning agents that are compatible with the topcoat.
None of these items is exotic. They are simply easier to collect before shipment than after installation, when a missing certificate can hold up a practical completion certificate for weeks.
Assemble the documentation package at order stage; recovering missing certificates after the membrane is tensioned is slow, expensive and sometimes impossible.
Matching the Fabric to the Application
Most enquiries that begin with a film specification end up in one of four application families once the budget is tested. Transportation work needs abrasion resistance and tear strength, and the truck cover range from 400 gsm rib-stop up to 900 gsm side curtain fabric covers that spread. Agricultural and aquaculture covers need UV stability plus resistance to ammonia and repeated folding. Leisure and event structures need colour consistency and flame performance. Inflatable structures need air retention, consistent coating on both faces and enough stiffness to hold a shape.
For inflatables specifically, the choice usually comes down to base cloth denier and coating weight. A 1,000 denier polyester base with an 850 gsm double-side coating is a sensible starting point for large-format inflatables that will be inflated, packed and reinflated many times over several seasons.
1000D 850gsm PVC Coated Fabric for InflatablesA heavy-duty 850 g/m² double-sided PVC fabric on 1000D polyester, suited to large inflatables and air-supported structures that need strength and repeated packing.View Product →
Where the structure is fixed rather than repeatedly packed, a lighter 650 gsm grade can reduce weight and cost without compromising the shape. The decision belongs with the fabricator who knows how the item will be handled on site, which is why application detail in the enquiry is worth more than a product code.
Handling and packing cycles decide the specification for inflatable and portable structures far more than nominal strength figures do.
FAQ: Made in USA ETFE and Coated Fabric Sourcing Questions
Is made in USA ETFE the only compliant option for a federally funded envelope?
Not automatically. Compliance depends on the specific domestic content rule, the tariff classification and how origin is determined for each component. Some projects accept a percentage-based approach, others apply stricter thresholds to the visible envelope only. Confirm the rule against your funding agreement before assuming either that film is mandatory or that an imported fabric is excluded.
Can coated PVC membrane replace ETFE cushions on an existing design?
Rarely on a like-for-like basis, because the structures are fundamentally different. Film works in pneumatic cushions on a light frame; coated fabric works in tension. A substitution usually means redesigning the frame and connections, and the structural savings that justified the film premium disappear in the process.
What documents should support an ETFE origin claim?
Ask for a certificate of origin, a mill certificate naming the extrusion facility, resin lot traceability and a separate statement identifying who welded the cushions. A single sentence on a quotation is not sufficient evidence for an auditor.
How much heavier is a coated PVC membrane than ETFE film?
Architectural film typically weighs roughly a third of a kilogram per square metre, while structural coated fabrics generally fall between 400 and 1,100 gsm depending on grade. That difference is why the supporting structure cannot simply be reused.
Can a manufacturer based in China supply into a US project?
Yes, for privately funded work and for scopes where the domestic content rule does not apply. For restricted scopes, a Chinese-origin fabric will usually not qualify, and buyers should plan a domestic or treaty-country source for those portions rather than assume an exemption will be granted.
What lead time should I plan for coated PVC fabric?
It depends on whether the colour and weight are stocked. Standard grades from current inventory move quickly; custom colours and non-standard grammages need additional production time. Ask for the lead time measured from deposit confirmation, and add time for inspection and freight.
Which coating should I choose for a fifteen-year appearance target?
A PVDF topcoat is the usual answer where cleaning access is limited or the envelope is highly visible. Acrylic coatings remain a defensible choice for shaded, low-profile or temporary structures where appearance is a lower priority than first cost.
Does Kingtex supply ETFE film?
No. Kingtex manufactures PVC-coated and laminated fabrics, including architectural membrane, cover material, inflatable fabric, mesh, tent fabric and truck cover fabric. Buyers who need film should source it from a specialist extruder and use a coated fabric where the duty cycle favours it.
The fastest way to resolve an origin-versus-performance debate is to have both suppliers document their claims in writing before the tender closes.
Where to Go Next
If the project is heading toward a coated fabric solution, the two most useful starting points are the application notes for architectural and construction work, and a direct conversation about your duty cycle with our technical team.
Architectural and construction applications How coated membrane is used in canopies, halls and tensile structures.
Talk to the technical team Share your load case, climate and handling profile for a specification proposal.
Sourcing decisions get easier once the question is framed correctly. Made in USA ETFE is a valid answer to a compliance problem, and on the right building it is also the right engineering answer. On a great many other buildings, a well-specified coated PVC membrane delivers the weather protection, the shading and the service life at a fraction of the cost, with a contractor base that can repair it locally for the next two decades.
Produits Associés
Nous invitons chaleureusement les clients nationaux et étrangers à visiter notre usine, à négocier une coopération et à créer ensemble un avenir radieux.
Coordonnées
- +86-13967331581
- +86-550-2356878
info@kingtexfabric.com
Adresse
- N°12, Route Weiyi, Zone de Développement Économique du Comté de Laian, Chuzhou, Anhui, Chine
Contactez-nous
Droits d'auteur ©Anhui Kingtex Material Technology Co, Ltd. Tous droits réservés.